
 |

Why Motorised Pulleys Make Sense in Harsh Mining and Quarrying Environments
Why motorised pulleys are well suited to demanding mining, quarrying and bulk handling conveyor applications. |
|
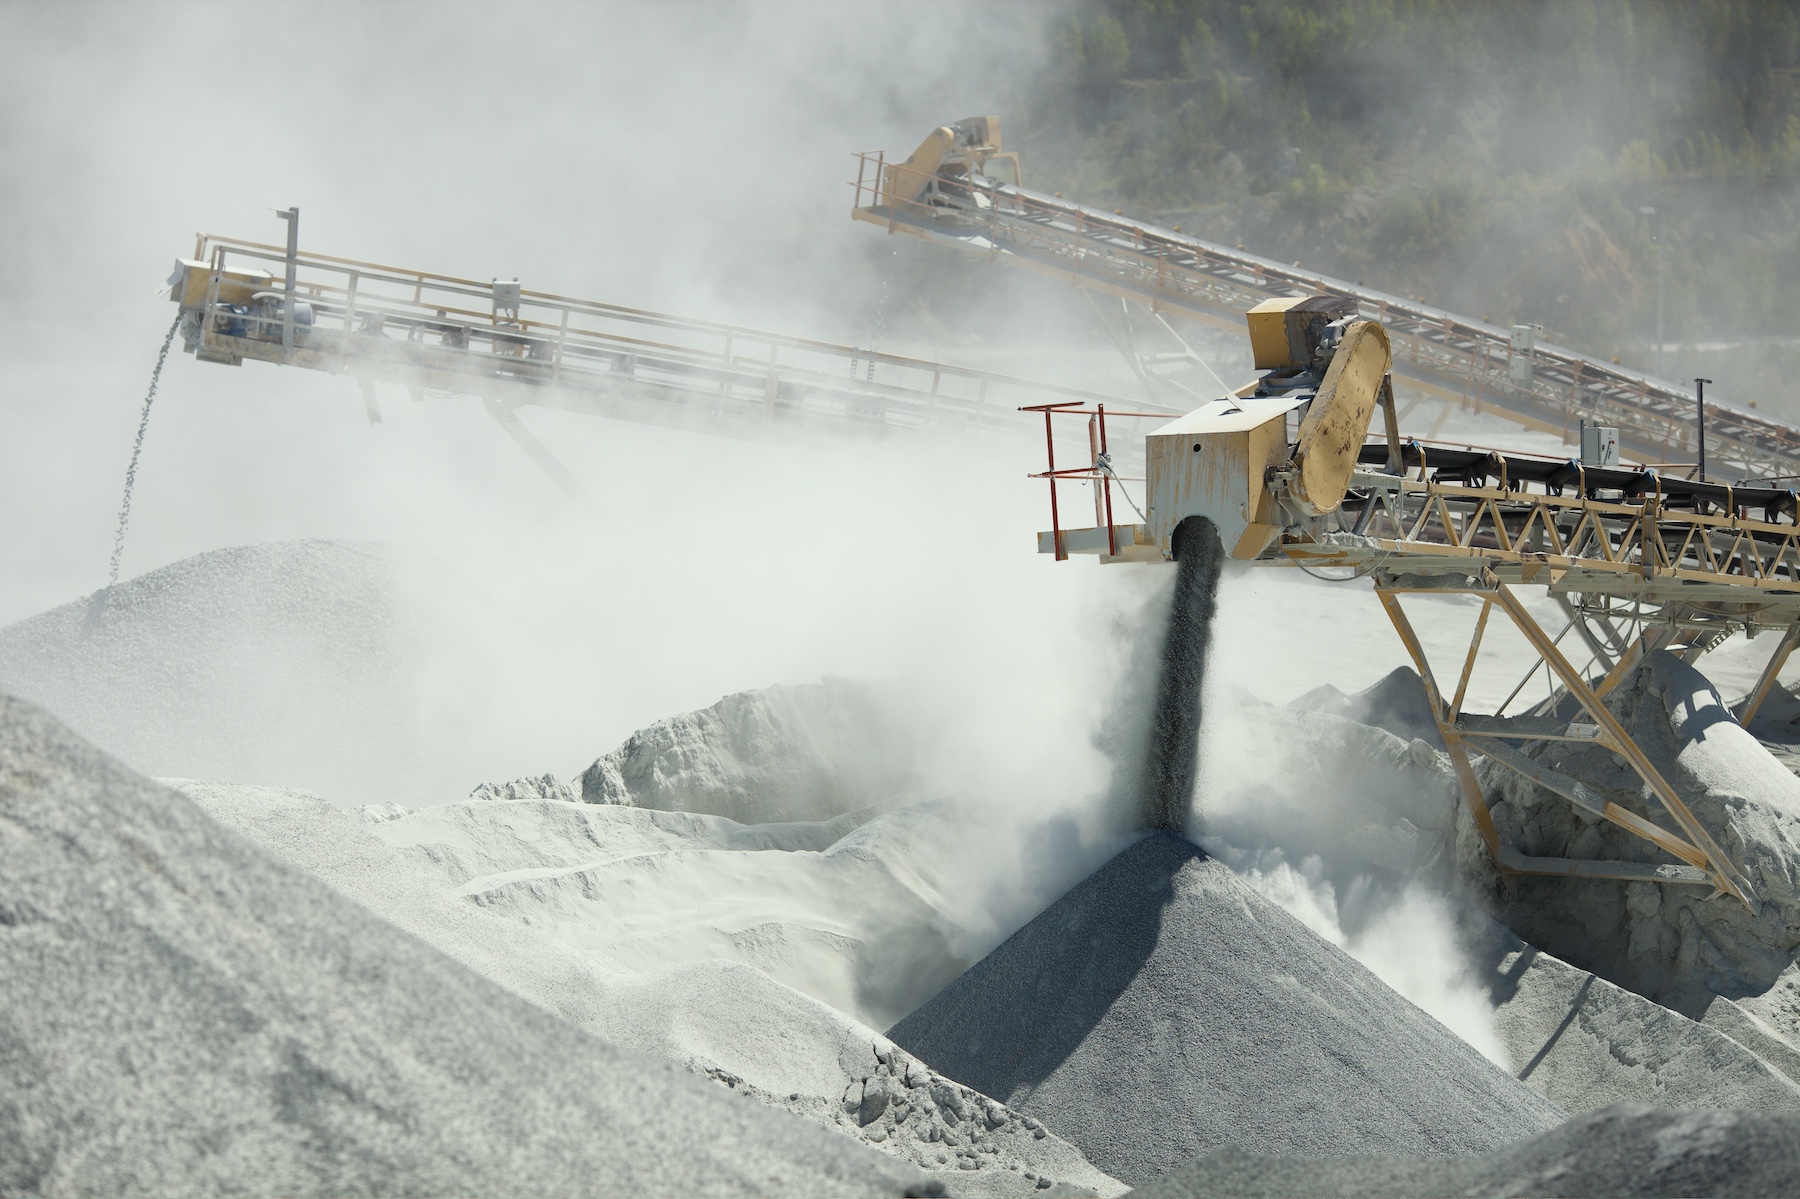
Mining and quarrying conveyors take a beating. Dust gets everywhere. Material spills. Water, mud and abrasive fines work their way into places you’d rather they didn’t, and many conveyors are expected to run for long shifts with very little tolerance for downtime. That puts the drive system under real pressure. A conventional external motor and gearbox arrangement can work perfectly well, but it also leaves more components sitting outside the conveyor where they’re exposed to the working environment. In a clean factory, that’s one thing. On a crusher, screen or quarry conveyor, it’s another. That’s where motorised pulleys make a lot of sense. 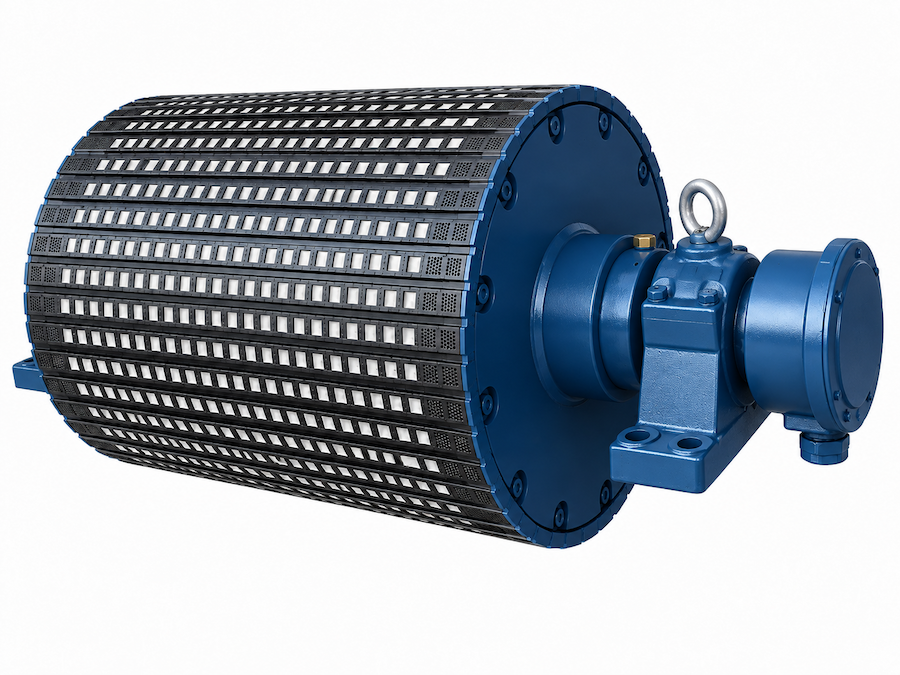 Heavy-duty motorised pulley for demanding mining, quarrying and bulk-handling conveyor applications.
A motorised pulley houses the electric motor and gearbox inside the pulley shell. That enclosed layout keeps the main drive components away from much of the dust, debris and general mess around the conveyor. On a quarry site, that matters. Fine material settles on exposed equipment, washdown introduces water and product spillage is part of daily life. The fewer vulnerable components you have sitting out in the open, the better. This is one of the biggest reasons motorised pulleys suit crushers, screening plants, mobile conveyors and other bulk-handling equipment. Less Hardware Around the Conveyor External drives bring extra hardware with them. You’ve got the motor, gearbox, couplings, shafts, mounting brackets and guarding to package around the conveyor. On a large fixed installation, that may be easy enough to accommodate. On mobile equipment, space disappears quickly. A motorised pulley removes a lot of that external hardware because the drive is built into the pulley itself. That gives design engineers a cleaner layout and, in many cases, makes it easier to fit the conveyor into the machine without having to create extra space for a side-mounted drive arrangement. For OEMs, that can simplify the design from the start rather than trying to squeeze the drive in at the end. 
Fewer Maintenance Points No conveyor drive is maintenance-free, and motorised pulleys shouldn’t be sold as if they are. What they do offer is a simpler external arrangement. With a conventional drive, couplings, shafts and other transmission components all need checking. Alignment matters. Guards have to be removed and refitted. Every extra component is another place where wear, contamination or damage can show up. With a motorised pulley, much of that external transmission hardware disappears. That’s useful on equipment working long hours or in areas where maintenance access isn’t great. Fewer exposed drive components generally means fewer things to inspect around the conveyor. For maintenance teams, that’s a practical benefit rather than a theoretical one. Specification Still Matters This is where mistakes get expensive. A motorised pulley has to be selected around the actual conveyor duty. Looking at motor power alone isn’t enough. Belt speed, torque, pulley diameter, belt tension, start-up conditions, operating hours and the environment all matter. A conveyor starting under a heavy load puts very different demands on the drive compared with one that starts empty and then runs continuously. Temperature matters too, especially in Australian mining and quarrying conditions. If those factors aren’t considered properly, the drive can be wrong even if the headline power rating looks right. 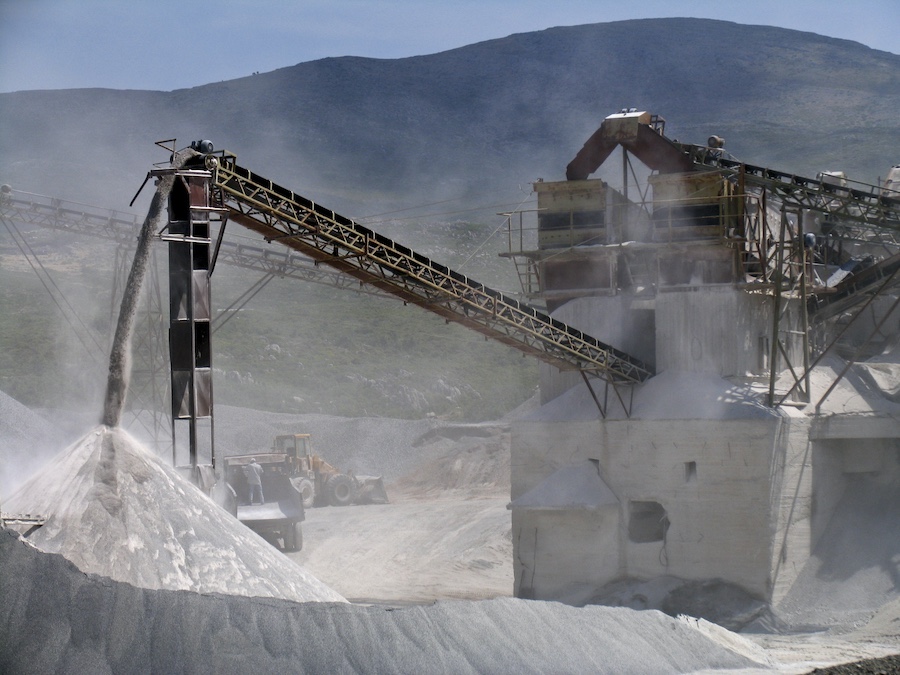
Motorised Pulleys for Mining and Quarrying Applications ATG Australasia supplies motorised pulleys for mining, quarrying and materials-handling applications across Australia and New Zealand. We work with OEMs, conveyor manufacturers, procurement teams and end users to understand the application before recommending a unit. That means looking at how the conveyor actually operates, not simply matching a motor size from a data sheet. If you’re designing a new conveyor, replacing an existing drive or reviewing a system that’s giving you problems, talk to the ATG Australasia team. Send us the conveyor details and working conditions. We’ll help you specify a motorised pulley that fits the application and the duty.
|